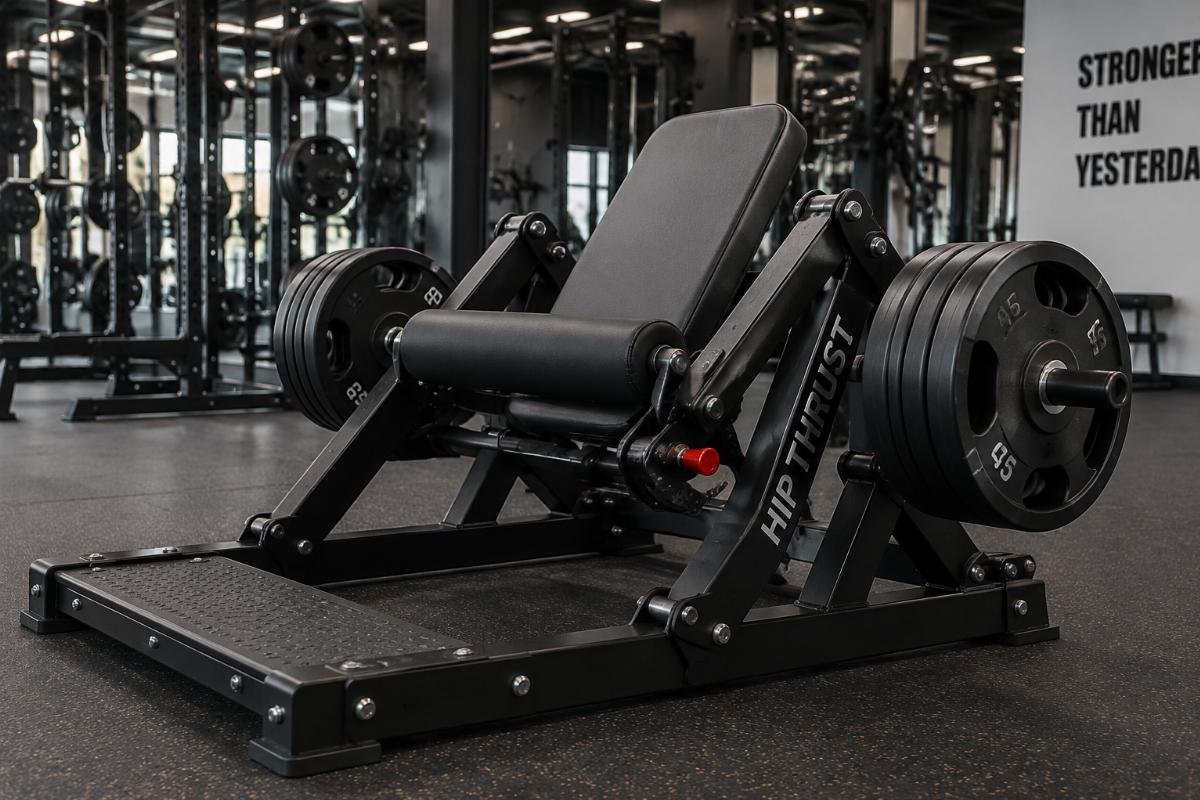

Plate-Loaded Functional Trainer for Multi-Site Gym Chain Wholesale Supplier
Most buyers assume plate-loaded equipment is simple enough to prevent batch-to-batch variation. The real culprit is unlocked mold revisions drifting tolerance stacks across production runs.
When outfitting a multi-location fitness chain, specification consistency across every Plate-Loaded Functional Trainer matters far more than unit price. Pin-insert feel, cable glide smoothness, and pulley bearing rotation must read identically from the first store to the last — otherwise member complaints and coach frustration multiply at every new opening.
I still remember a shipment bound for Riyadh. The first sample batch rolled off the line with pulley stacks, cable guides, and weight-horn rails all within spec. Then the second full container arrived, and during on-site installation the pin-insert holes on the weight stacks were misaligned by a few millimeters — the factory had swapped a stamping die without notification. Coaches at multiple locations reported the pins jamming during load changes. That single oversight forced a field retrofit across several stores. Since then, I treat mold-lock confirmation and per-container pin-hole sampling as non-negotiable checkpoints for any multi-site order. [NEED_CITE: root causes of batch variation in plate-loaded strength equipment per IHRSA procurement guidelines]
Specification drift is rarely visible in photos or spec sheets, which is why multi-site buyers need a structured approach to sourcing a Plate-Loaded Functional Trainer that performs identically across locations.
Why Specification Consistency Matters More Than Price for Multi-Site Gyms?
A fitness chain sells repeatable experience — a member walking into any branch expects the same resistance feel, the same pin insertion, the same cable glide. When a Plate-Loaded Functional Trainer behaves differently from one store to the next, the brand promise breaks before the member even finishes the warm-up set. [NEED_CITE: member retention impact of equipment consistency in multi-site fitness operations]
A Middle East chain operating across multiple cities learned this the hard way. Their initial sample approval went smoothly. But once full containers reached the second and third locations, coaches noticed the weight-stack pins required noticeably more force to insert. The root cause: an unlocked die change had shifted hole-position tolerance beyond acceptable range. The buyer had compared unit prices across suppliers but had not locked mold-revision control into the purchase agreement.
The hidden cost is not just the replacement parts. It includes coach re-training, member complaints, and the reputational damage of opening a new branch with equipment that feels "off." For a Plate-Loaded Functional Trainer deployed across a chain, every unit must share the same resistance curve, the same pin-detent click, and the same cable stack smoothness. [NEED_CITE: EN ISO 20957 safety and performance requirements for plate-loaded strength equipment]
What Are the Hidden Quality Risks in Plate-Loaded Functional Trainers?
Three failure modes hide behind a clean-looking exterior: pin-insert hole tolerance, pulley bearing smoothness, and cable glide resistance under load. None of these show up in a catalog photo, yet each directly shapes how the Plate-Loaded Functional Trainer feels during a working set.
- Pin-insert hole tolerance. If the stamping die shifts even slightly, the guide-rod holes on the weight stack drift out of alignment. Pins insert smoothly on the sample but jam on production units. The difference between a controlled die and an unlocked one is the gap between a clean click and a stuck plate. [NEED_CITE: stamping die tolerance standards for fitness equipment weight stacks]
- Pulley bearing rotation. A Southeast Asian chain received multiple containers of the same Plate-Loaded Functional Trainer model and noticed that pulleys on later batches spun with perceptibly more friction. The bearing supplier had been substituted without disclosure. Coaches at the newer locations reported a "gritty" pull compared to the flagship store.
- Cable glide under load. Empty-cable pull may feel fine, but once plates are loaded, friction compounds through every pulley in the stack. A cable that passes empty-load QC can still fail under working weight if the housing alignment or pulley groove depth is inconsistent.
| Risk Point | Sample-Batch Behavior | Unlocked Production Drift |
|---|---|---|
| Pin-insert hole alignment | Clean detent engagement | Noticeably tighter or misaligned |
| Pulley bearing rotation | Smooth free-spin | Perceptible drag under load |
| Cable glide (loaded) | Consistent resistance | Friction variance across units |
| Powder-coat color match | Approved RAL reference | Visible shade shift between batches |
How to Lock Down Mold Changes and Prevent Batch Variations?
The single most effective control is a written mold-lock clause tied to every production run of the Plate-Loaded Functional Trainer. Without it, the factory is free to substitute dies, bearing suppliers, or cable vendors between containers — and none of these changes appear on a commercial invoice.
The process works in layers:
- Die registration at sample approval. When the sample is signed off, record the exact die ID used for weight-stack plates, pin holes, and frame weld jigs. This becomes the baseline reference for all future containers. [NEED_CITE: mold-lock and traceability best practices in commercial fitness equipment manufacturing]
- Written change-notification requirement. Any die replacement, bearing supplier switch, or cable vendor change must be disclosed in writing before production begins. The buyer holds approval rights — not the factory’s production scheduler.
- Per-container pin-hole sampling. On every container of a Plate-Loaded Functional Trainer, pull a statistical sample of weight-stack plates and verify pin-hole alignment with a go/no-go gauge. This catches drift before the container leaves the port.
- Batch-traceability tagging. Each unit shipped should carry a production-batch code traceable back to the die set, bearing lot, and cable lot used. When a field complaint arises, the buyer can identify whether it is an isolated unit or a full-batch issue.
A Middle East buyer with a growing chain adopted this protocol after the pin-hole incident. For every subsequent container of the Plate-Loaded Functional Trainer, the factory provided a batch traceability sheet alongside the packing list. When a later shipment showed a slight color variation on the frame, the batch code pinpointed the powder-coat lot — and the supplier replaced the affected units under the traceability commitment rather than disputing the claim.
What Quality Control Protocol Should Multi-Site Buyers Implement?
Visual inspection catches paint defects; functional inspection catches the problems that actually frustrate coaches and members. A multi-site buyer needs a QC protocol for the Plate-Loaded Functional Trainer that goes well beyond counting cartons and checking weld seams.
The functional protocol should cover three layers:
- Pin-insert feel test. Using a go/no-go gauge or a reference pin, verify that the weight-stack pin slides in and detents cleanly on every sampled unit. The standard is not "it fits" — it is "it feels identical to the approved sample." [NEED_CITE: functional testing methods for selectorized and plate-loaded weight stacks]
- Loaded cable glide test. Load the stack to a working weight and pull through the full range of motion. The resistance should be smooth, with no binding, stuttering, or lateral cable rub. An empty-cable pull alone will miss housing misalignment that only appears under load.
- Pulley bearing noise and rotation check. Spin each pulley by hand and listen for grit or roughness. Under the EN ISO 20957 framework, bearing assemblies must sustain repeated cycling without degradation — but the real-world check is whether a new unit feels the same as the sample approved months earlier. [NEED_CITE: EN ISO 20957 bearing durability and smoothness requirements]
A Southeast Asian chain introduced this three-layer protocol after receiving containers where the pulleys felt noticeably different from the flagship store’s equipment. The protocol caught a bearing-substitution issue before the affected units were distributed across locations. The factory reverted to the originally approved bearing supplier, and subsequent containers matched the original feel.
How to Build a Long-Term Partnership with Reliable Fitness Equipment Suppliers?
The right supplier for a multi-site chain is not the one offering the lowest unit price — it is the one willing to lock molds, trace batches, and guarantee color and feel consistency on reorder. A Plate-Loaded Functional Trainer sourced for a chain is not a one-time purchase; it is a recurring commitment that spans years of expansion and replacement.
A reliable partner demonstrates three behaviors:
- Mold-lock discipline. The factory treats the approved sample’s die set as a controlled baseline and refuses to substitute without written buyer approval. This is not a convenience — it is the foundation of multi-site consistency.
- Batch-level traceability. Every Plate-Loaded Functional Trainer shipped carries a code linking it to the production lot, bearing supplier, cable lot, and powder-coat batch. When a reorder arrives eighteen months later, the buyer can verify that the new units match the original specification — not just on paper, but in pin feel, cable glide, and color shade. [NEED_CITE: supplier traceability and reorder consistency standards in commercial fitness equipment]
- Reorder color and finish matching. Powder-coat color shifts subtly between batches, especially when the coating supplier changes. A committed partner maintains a signed RAL reference panel and runs spectrophotometer checks against it on every reorder of the Plate-Loaded Functional Trainer, ensuring that a unit added to a new location does not look like it belongs to a different brand.
A buyer operating across multiple regions found that switching to a supplier with these disciplines eliminated the recurring headaches of mismatched equipment across sites. Reorders of the Plate-Loaded Functional Trainer arrived with the same pin feel, the same cable smoothness, and the same frame color as the original deployment — and the coaches stopped fielding member complaints about "the machine that feels different."
Conclusion
Multi-site gym procurement succeeds or fails on consistency, not unit cost. Locking mold revisions, sampling pin-hole tolerance per container, and running functional QC on loaded cable glide and bearing smoothness transform a Plate-Loaded Functional Trainer from a commodity purchase into a repeatable brand experience across every location.